Quality Assurance & Testing Protocol
Every industrial roller built at Mishree Engineers passes through rigorous multi-stage metrology, ultrasonic inspection, dial indicator runout checks, Shore durometer verification, and computerized dynamic balancing.
Our Transparent Quality Philosophy
In high-speed continuous manufacturing, an industrial roller is only as reliable as its tightest tolerance. A mere 0.05 mm concentricity error or minor static unbalance can lead to severe machine vibration, premature bearing failure, uneven web tension, or surface creasing on sensitive films and fabrics.
Established in 2018 in Ahmedabad's Akshar Industrial Park, Mishree Engineers upholds a direct, data-backed quality standard: we verify every dimensional parameter with calibrated instruments and provide real inspection certificates with every dispatch.
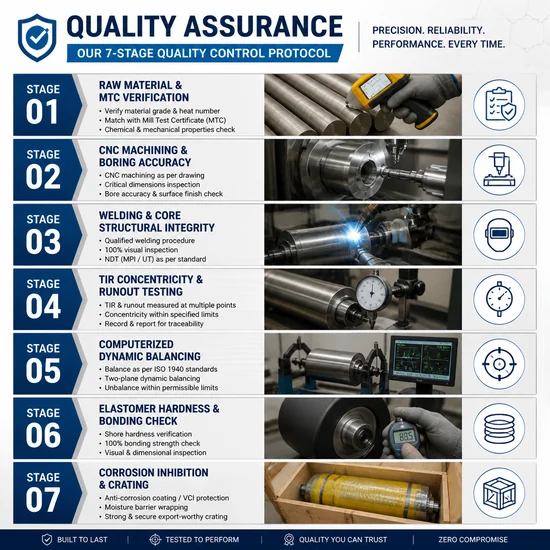
Our 7-Stage Quality Control Protocol
From raw steel receipt to final wooden crate dispatch, nothing leaves our shop unmeasured.
Raw Material & MTC Verification
All heavy-wall steel pipes (IS 2062, ST 52, ASTM A106), stainless steel tubes (SS 304, SS 316), and shaft rounds (EN8, EN19, EN24) are inspected against Mill Test Certificates (MTC).
- Chemical composition and yield strength verification
- Ultrasonic thickness testing of seamless pipe walls
- Visual inspection for seam inclusions, pitting, or ovality
CNC Machining & Boring Accuracy
Precision turning, facing, and internal boring operations on heavy-duty CNC lathes are checked against approved engineering drawings.
- Shaft journal diameters verified to ISO h6 / k6 tolerances
- Three-point internal bore micrometers for bearing seat accuracy
- Stress relief fillets machined on all shaft transition steps
Welding & Core Structural Integrity
End hub disks and flanges are welded with full penetration MIG/TIG processes to eliminate rotational shear stresses.
- Pre-heating on thick alloy hubs to prevent weld cracking
- Liquid penetrant (Dye Penetrant / DP) testing of circumferential weld seams
- Post-weld thermal stress relief to eliminate residual distortion
TIR Concentricity & Runout Testing
Rollers are placed on precision ground V-blocks or mounted between live headstock and tailstock centers to measure Total Indicator Runout (TIR).
- Calibrated Dial Test Indicators (0.001 mm resolution) applied
- Runout verified at 5 points: journals, ends, and barrel center
- Standard tolerance TIR < 0.03 mm to 0.05 mm across total length
Computerized Dynamic Balancing
Critical high-speed and process rollers undergo dual-plane dynamic balancing on our computerized balancing rig.
- Balanced to ISO 1940-1 Grade G2.5 (precision) or G6.3 (standard)
- Correction weights welded internally or added via set screws
- Residual unbalance measured and logged in gram-millimeters (g-mm)
Elastomer Hardness & Bonding Check
Rubber, Polyurethane, and Teflon coated rollers undergo non-destructive and sample destructive property verification.
- Shore A & Shore D durometer testing across 5 surface zones
- Adhesion check between elastomer and blasted/primed metal core
- Surface roughness (Ra) measurement with portable stylus tester
Corrosion Inhibition & Crating
Before dispatch, every roller is cleaned, sealed, and packaged to ensure zero transit damage or atmospheric oxidation.
- Heavy-duty de-watering rust preventive oil applied to journals
- VCI anti-corrosion stretch film and shock-absorbent cushioning
- Custom wooden crates with dedicated journal saddle supports
Quality Documentation Supplied With Every Batch
Full traceability for plant managers, quality directors, and EPC procurement engineers.
| Document / Report | Parameters Recorded | Applicable Standard |
|---|---|---|
| Pre-Dispatch Inspection Report (PDIR) | Barrel OD, face length, shaft step diameters, keyway depth/width, bearing journal tolerances | ISO 286 / Client Drawing Blueprint |
| Dynamic Balancing Certificate | Operating RPM, balance test RPM, balance plane A & B residual unbalance (g-mm), balancing grade | ISO 1940-1 Grade G2.5 / G6.3 |
| Total Indicator Runout (TIR) Log | Dial indicator readings across journals, barrel shoulders, and mid-span | TIR ≤ 0.03 mm Standard |
| Hardness Verification Sheet | Shore A or Shore D durometer readings recorded at 5 longitudinal barrel positions | ASTM D2240 / ISO 868 |
| Surface Roughness (Ra) Report | Digital surface stylus measurements (Ra, Rz, Rmax) | ISO 4287 / ASME B46.1 |
| Raw Material Mill Test Report (MTC) | Chemical composition (C, Mn, Si, P, S, Cr, Ni) and mechanical tensile / yield strengths | EN 10204 3.1 Certification |
Third-Party Inspection (TPI) Welcomed
Mishree Engineers routinely accommodates customer-appointed Third-Party Inspection (TPI) agencies before final crating and dispatch. We maintain calibrated instruments, granite inspection tables, and test rigs ready for inspector review.
We regularly collaborate with major domestic and international inspection agencies including:
- TÜV SÜD / TÜV Rheinland
- SGS India
- Bureau Veritas
- DNV GL
- Customer Quality Assurance Engineers & Auditors
Schedule an On-Site Plant Inspection
Are you an OEM machine builder, EPC contractor, or plant procurement team in Gujarat or visiting Ahmedabad? We welcome client technical teams to witness dynamic balancing and dimensional inspection at our facility.
Factory Address:
21, Akshar Industrial Park, GIDC Road,
Ahmedabad – 382445, Gujarat, India
Quality Assurance FAQs
In a rotating cylinder, even minor variations in pipe wall thickness or slight shaft eccentricity create centrifugal forces that increase with the square of rotation speed ($F = m \cdot \omega^2 \cdot r$). At high line speeds, unbalance causes intense vibration, rapid bearing wear, structural fatigue in machine frames, and visible chatter marks or thickness variations on web materials like films, textiles, and paper. Dynamic balancing according to ISO 1940 eliminates this parasitic vibration.
We achieve tight concentricity by machining shafts and end-caps with precision press-fit tolerances, welding hubs with balanced rotational sequence passes, and taking the final outer diameter skimming cut or grinding pass while the roller is mounted directly on its own turned shaft centers. This ensures the barrel rotation axis is mathematically identical to the bearing journal axis.
Our internal Non-Conformance Protocol segregates any part failing dimensional, TIR, or hardness parameters immediately. Parts cannot be dispatched unless they meet drawing specifications. Non-conforming elastomer coverings are stripped and re-vulcanized, while out-of-tolerance shafts or shells are rejected and remachined from fresh raw material.
Yes. All micrometers, verniers, bore gauges, dial test indicators, durometers, and surface roughness testers are calibrated against NABL-accredited master reference gauges on a scheduled calibration cycle, with records maintained in our inspection room.